Choosing the right Steel Round Tube starts with the job it must perform. A greenhouse frame, a handrail, and a machine support may use similar-looking tubing, yet face very different loads and conditions. Wall thickness, outside diameter, steel grade, and finish all matter. So does the way the tube will be cut, welded, or joined.
A reliable selection begins with measurable requirements. Check the expected load, span, exposure to moisture, and available connection details. For example, a tube beside a damp loading bay may need a different corrosion-protection plan than one inside a dry workshop. Ask suppliers for grade, dimensions, tolerances, and relevant test documentation. Then compare those details against the design requirements—not just the price per length. Small differences matter.
One caution: no source article or verifiable expert quotation was provided, so I will not invent an expert’s name or words. A qualified materials engineer or structural designer can review unusual loads, safety-critical uses, and uncertain specifications. That review may feel like extra work. It can prevent a costly mismatch. This guide will help you compare the key factors, while recognizing that a general checklist cannot replace project-specific engineering judgment.
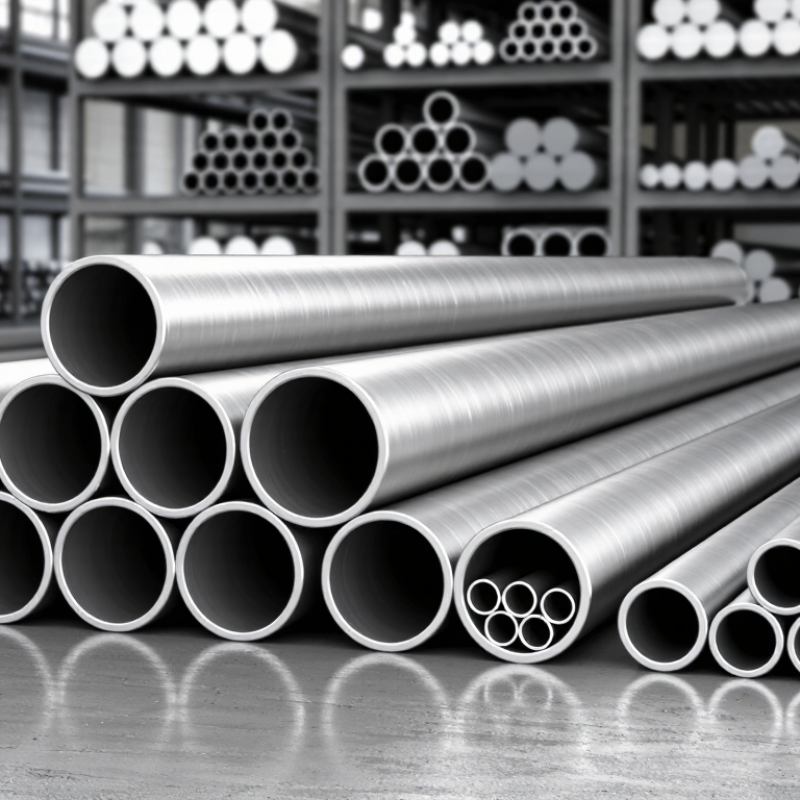
Start by defining what the tube must do. A guardrail post, equipment frame, and long-span support face different load cases. Identify whether loads act in compression, bending, tension, or torsion, and note where they enter the tube. Loads rarely act alone. Include the tube’s unsupported length, connection details, expected vibration, and exposure to moisture.
ASTM A500 grades help narrow the choice, but grade alone does not determine capacity. For round tubing, Grade B has a specified minimum yield strength of 42 ksi, while Grade C is 46 ksi; Grade A is 33 ksi. These are minimum material properties, not allowable design stresses. A stronger grade may help, yet a thin wall or long unsupported span can still make a tube unsuitable. Check the applicable ASTM edition and the material test report.
Compare outside diameter and wall thickness against the actual design loads. A larger diameter can improve resistance to bending, while added wall thickness may help with local damage and connection forces. Measure the real span. Account for holes, welds, end supports, and corrosion allowance where relevant. One easy mistake is choosing by grade name alone; I would question that choice until dimensions and load assumptions are checked. For critical structures, have a qualified engineer verify the calculations and applicable design requirements.
Choosing a steel round tube starts with the job it must do. Measure the outside diameter and wall thickness, then check how the tube will be supported and connected. A larger diameter can improve resistance to bending, while a thicker wall adds material and weight. It may also affect fit. Small details matter.
Steel’s density is commonly estimated at 7,850 kg/m³. To estimate tube mass, convert dimensions to metres and multiply the steel cross-sectional area by the tube length and density. For a 50 mm outside diameter tube with a 3 mm wall, the inside diameter is 44 mm. A two-metre length weighs about 7 kg, before accounting for manufacturing tolerances or coatings. That is an estimate, not a scale reading.
Use the figure to compare options and check handling loads. Density alone does not tell you whether a tube is strong enough; grade, span, loading, welds, and support conditions matter too. I still recheck unit conversions, because millimetres entered as metres can distort a calculation badly. Not quite obvious. For structural or safety-critical work, verify the design against applicable engineering requirements and supplier data.
ASTM A500/A500M lists minimum yield strengths of about 290 MPa for Grade B and 315 MPa for Grade C round structural tubing. That is an 8.6% increase. Useful, but not a free pass. In a frame supporting a small platform, the higher grade may provide more capacity at the same tube size, depending on the design. The actual benefit still depends on wall thickness, diameter, unsupported length, connections, and loading. AISC 360-22 design provisions likewise require engineers to consider member geometry and stability, not yield strength alone.
For a tube exposed to bending or compression, compare the specified yield strength with the calculated demand and the required safety factors. Check the mill test report, too; nominal grade alone does not verify a delivered tube’s dimensions or properties. A common selection error is choosing Grade C and then reducing wall thickness without checking buckling or connection behavior. That can erase the expected advantage. Grade B may suit a lighter-duty member when the design checks pass. Grade C can be worthwhile when its added strength addresses a documented demand. Not always. I would verify the governing load case and fabrication details before paying for the higher grade. Sources: ASTM A500/A500M, mechanical-property requirements; AISC 360-22, Specification for Structural Steel Buildings.
Choose a steel round tube by the dimensions the assembly actually needs, not its nominal label. Check outside diameter, wall thickness, ovality, straightness, and end squareness against the relevant product specification. A tube that fits a bracket at one end may bind at the other. Small differences matter. Confirm whether tolerances apply before or after coating, because added thickness can affect close-fit joints.
Map the real corrosion exposure: indoor condensation, road salt, coastal spray, or industrial moisture. NACE International’s IMPACT study estimated global corrosion costs at US$2.5 trillion annually, about 3.4% of global GDP, using 2013 estimates. That is not a tube-specific forecast, but it shows why exposure deserves attention. ISO 9223 corrosivity categories can help frame atmospheric conditions; sheltered joints and standing water still need separate consideration.
Match the coating to that exposure and the tube’s service life. Specify surface preparation, coating type, thickness, and repair method for cut ends or damaged areas. A bright finish proves little. For hot-dip galvanizing, check the applicable coating specification and confirm that venting and drainage suit the tube’s shape. I may be overcautious, but coating thickness is easy to overlook when clearance is tight. A small trial fit can reveal problems before fabrication scales up.
| Selection Check | What to Specify or Measure | Practical Guidance | Why It Matters |
|---|---|---|---|
| Outside diameter (OD) | Nominal OD and permitted tolerance; measure at several points around the tube and along its length. | Confirm the tolerance in the applicable product standard and purchase specification. Check whether the measurement is taken before or after coating. | OD affects fit in sleeves, clamps, bearings, and mating parts. |
| Wall thickness | Nominal wall thickness, minimum acceptable thickness, and the specified tolerance. | State whether the design depends on nominal or minimum wall thickness. Use the relevant tube standard because permitted tolerances vary by specification, size, and manufacturing process. | Wall thickness influences load capacity, stiffness, weight, and corrosion allowance. |
| Length and end condition | Cut length tolerance, end squareness, burr limits, and any bevel or end-preparation requirements. | For assemblies, define the finished cut length and whether coating buildup is included in the dimension. | Consistent ends and lengths simplify assembly and reduce rework. |
| Straightness and ovality | Maximum permitted bow and out-of-roundness, as defined by the governing specification or drawing. | Check straightness over the required reference length. For rotating, sliding, or close-fitting parts, set explicit limits rather than relying on a general description. | Excessive bow or ovality can prevent proper fit, alignment, or movement. |
| Dry indoor exposure | Expected humidity, condensation, cleaning chemicals, and contact with other materials. | Uncoated carbon steel may be suitable in controlled, dry conditions if occasional surface rust is acceptable and maintenance is planned. | Even indoor steel can corrode where moisture, condensation, or chemical residues are present. |
| Outdoor or wet exposure | Rain, standing water, humidity, temperature changes, and whether the tube can drain and dry. | Consider a corrosion-protective coating such as hot-dip galvanizing or a compatible paint system. Specify surface preparation, coverage, and repair of damaged areas. | Repeated wetting and retained moisture accelerate corrosion of unprotected carbon steel. |
| Marine, de-icing salt, or chemical exposure | Salt spray or splash, chemical identity and concentration, temperature, and cleaning regime. | Do not select a coating or stainless grade from the exposure label alone. Confirm suitability for the actual environment; obtain corrosion-engineering guidance for severe or chemical service. | Chlorides and some chemicals can cause rapid coating breakdown or localized corrosion, including pitting of some stainless steels. |
| Hot-dip galvanized coating | Coating standard, required coating thickness or mass, coverage, and treatment of cut edges or repairs. | Suitable for many outdoor applications when the coating is specified for the service environment. Account for coating buildup where close dimensional fit is required. | Zinc provides a barrier and sacrificial protection to steel; coating thickness and service life depend on exposure. |
| Paint or powder coating | Surface preparation, primer and topcoat system, dry-film thickness, edge coverage, and repair procedure. | Use a coating system rated for the exposure and apply it to properly prepared steel. Protect cut edges, welds, and damaged areas according to the coating specification. | Performance depends on preparation, coating continuity, and maintenance—not just the coating name. |
| Stainless steel option | Grade, product specification, surface finish, weld condition, and exposure to chlorides or chemicals. | Select the grade for the environment and fabrication requirements. Stainless steel is not immune to corrosion; avoid assuming that any stainless grade is suitable for marine or chemical service. | Appropriate stainless grades can reduce maintenance, but incorrect selection or contaminated surfaces can still corrode. |
| Purchase-order verification | Tube standard and grade, dimensions and tolerances, length, coating system, inspection requirements, and material test documentation. | Use one consistent unit system, identify the measurement method where needed, and require documentation appropriate to the application. | Clear requirements help ensure the delivered tube matches the design and the intended service conditions. |
How to Choose the Right Steel Round Tube?
Verify ASTM Compliance, Mill Test Certificates, and Inspection Records
A tube’s ASTM claim should identify the exact specification and grade, not just say “ASTM compliant.” Check that the cited standard and edition match your purchase requirements. Small details matter. The mill test certificate (MTC) should link the tube to a heat number and report relevant chemistry and mechanical properties. Compare those values with the specification, including yield strength and tensile strength where required. Also confirm the listed outside diameter and wall thickness match the ordered dimensions. A neat certificate is useful, but it cannot fix a mismatch.
Inspection records add evidence beyond the MTC. Look for dated dimensional checks, visual inspection results, and any required non-destructive testing. Confirm measuring equipment was within calibration and that the records identify the inspected lot. On delivery, compare tube markings and bundle tags with the heat numbers on the paperwork. If they differ, pause acceptance and ask for traceable clarification. No document set catches every flaw. That is worth remembering. A quick spot check with calipers may reveal an issue the paperwork does not show, though it should not replace the agreed inspection plan.